Technology & equipment
A complete machine park under one roof
From the first cut to the final dimensional check, every step of making tools and precision parts happens on our own machines.
- Production area
- 3,000 m²
- Machines
- 50+
- Best tolerance
- ±0.001 mm
- Press capacity
- 600 t
Machine park
What we work with
Turning, milling, grinding, jig boring, EDM, cutting, pressing and heat treatment — combined in one controlled process.
-
01
Turning
CNC and universal lathes for shaft and flange parts.
- Structural and tool steels, stainless steels and non-ferrous metals
- Punches, guides, bushings and other cylindrical tool elements
- Fine turning combined with grinding for tight tolerances
-
02
Milling
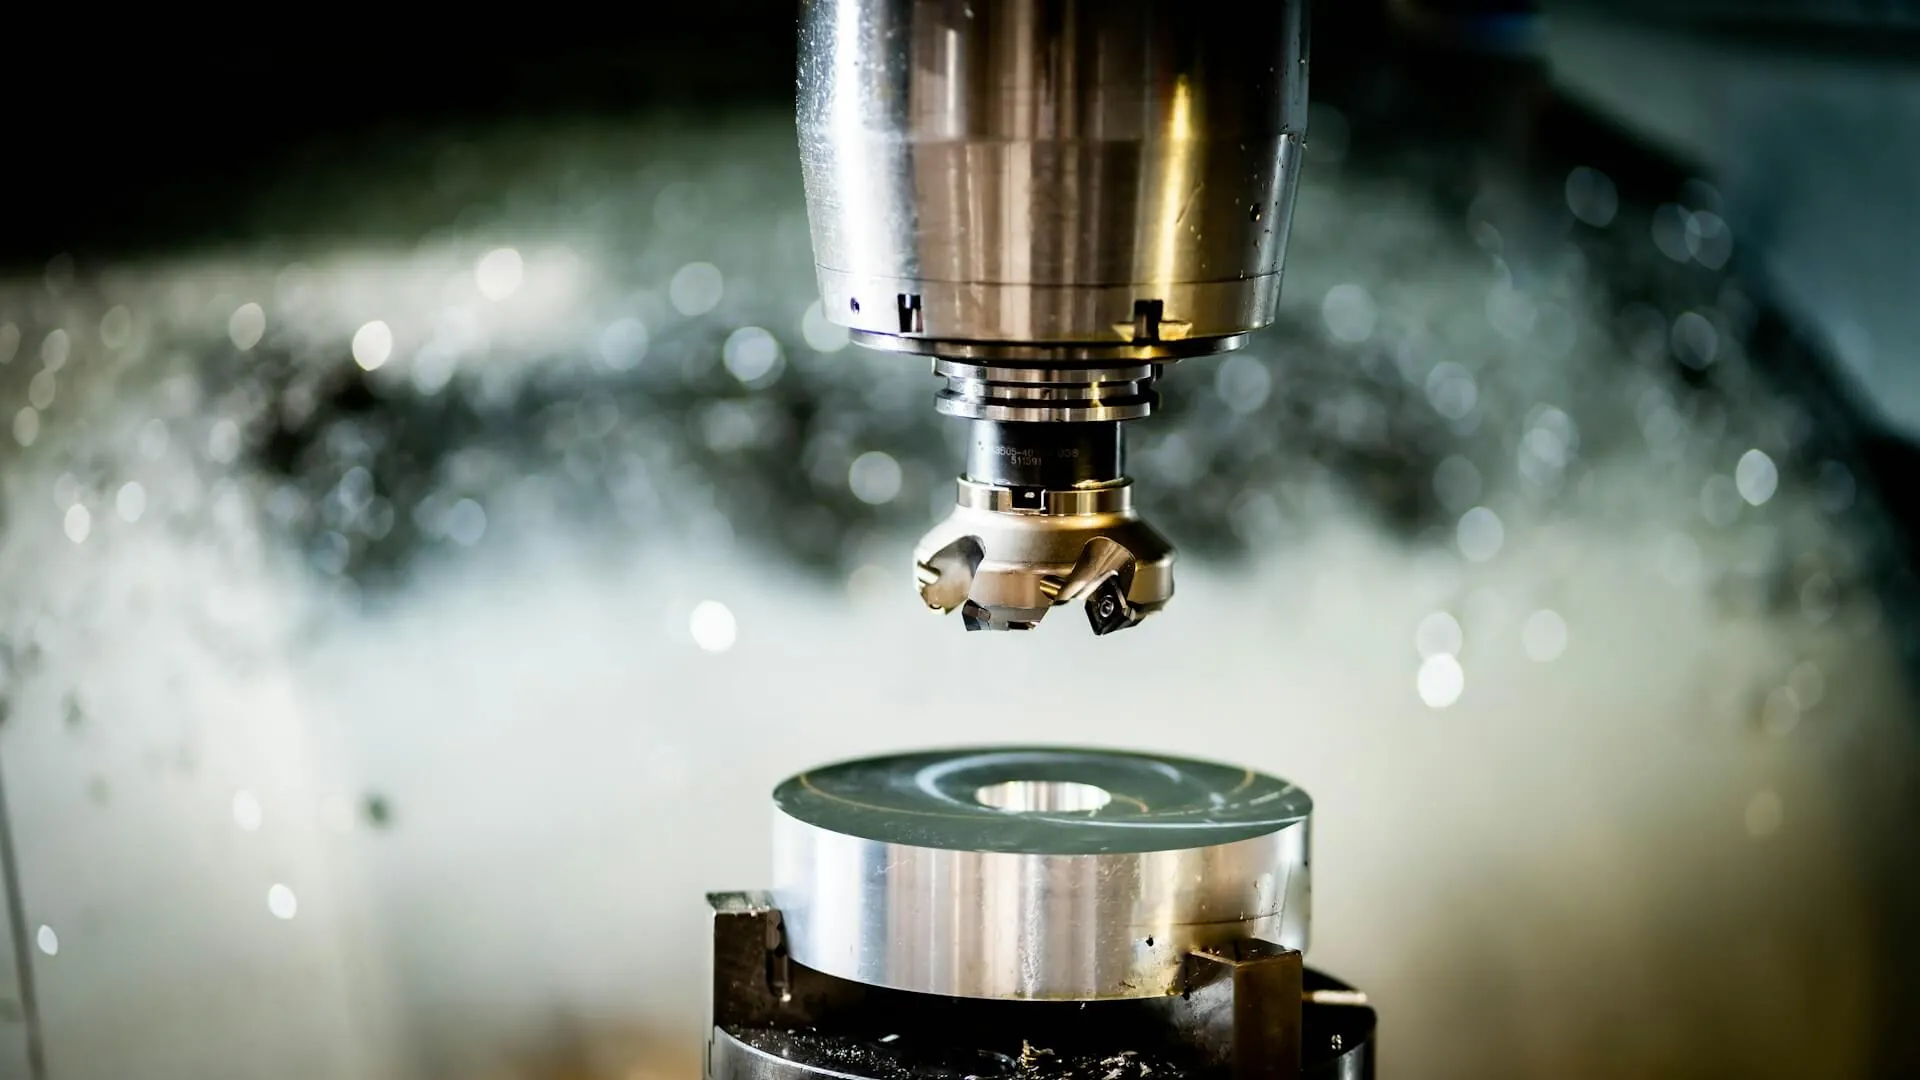
CNC and conventional milling machines for plate and profiled parts.
- 3-axis CNC milling up to 800 × 550 × 550 mm
- Conventional milling up to 500 × 600 × 1,000 mm
- Slots, stepped surfaces and precision fits
-
03
Grinding
Finishing of guides, plates, punches and other active tool elements.
- Surface and cylindrical grinding
- External, internal and centerless grinding
- Polishing of round and flat surfaces
-
04
Jig boring & jig grinding
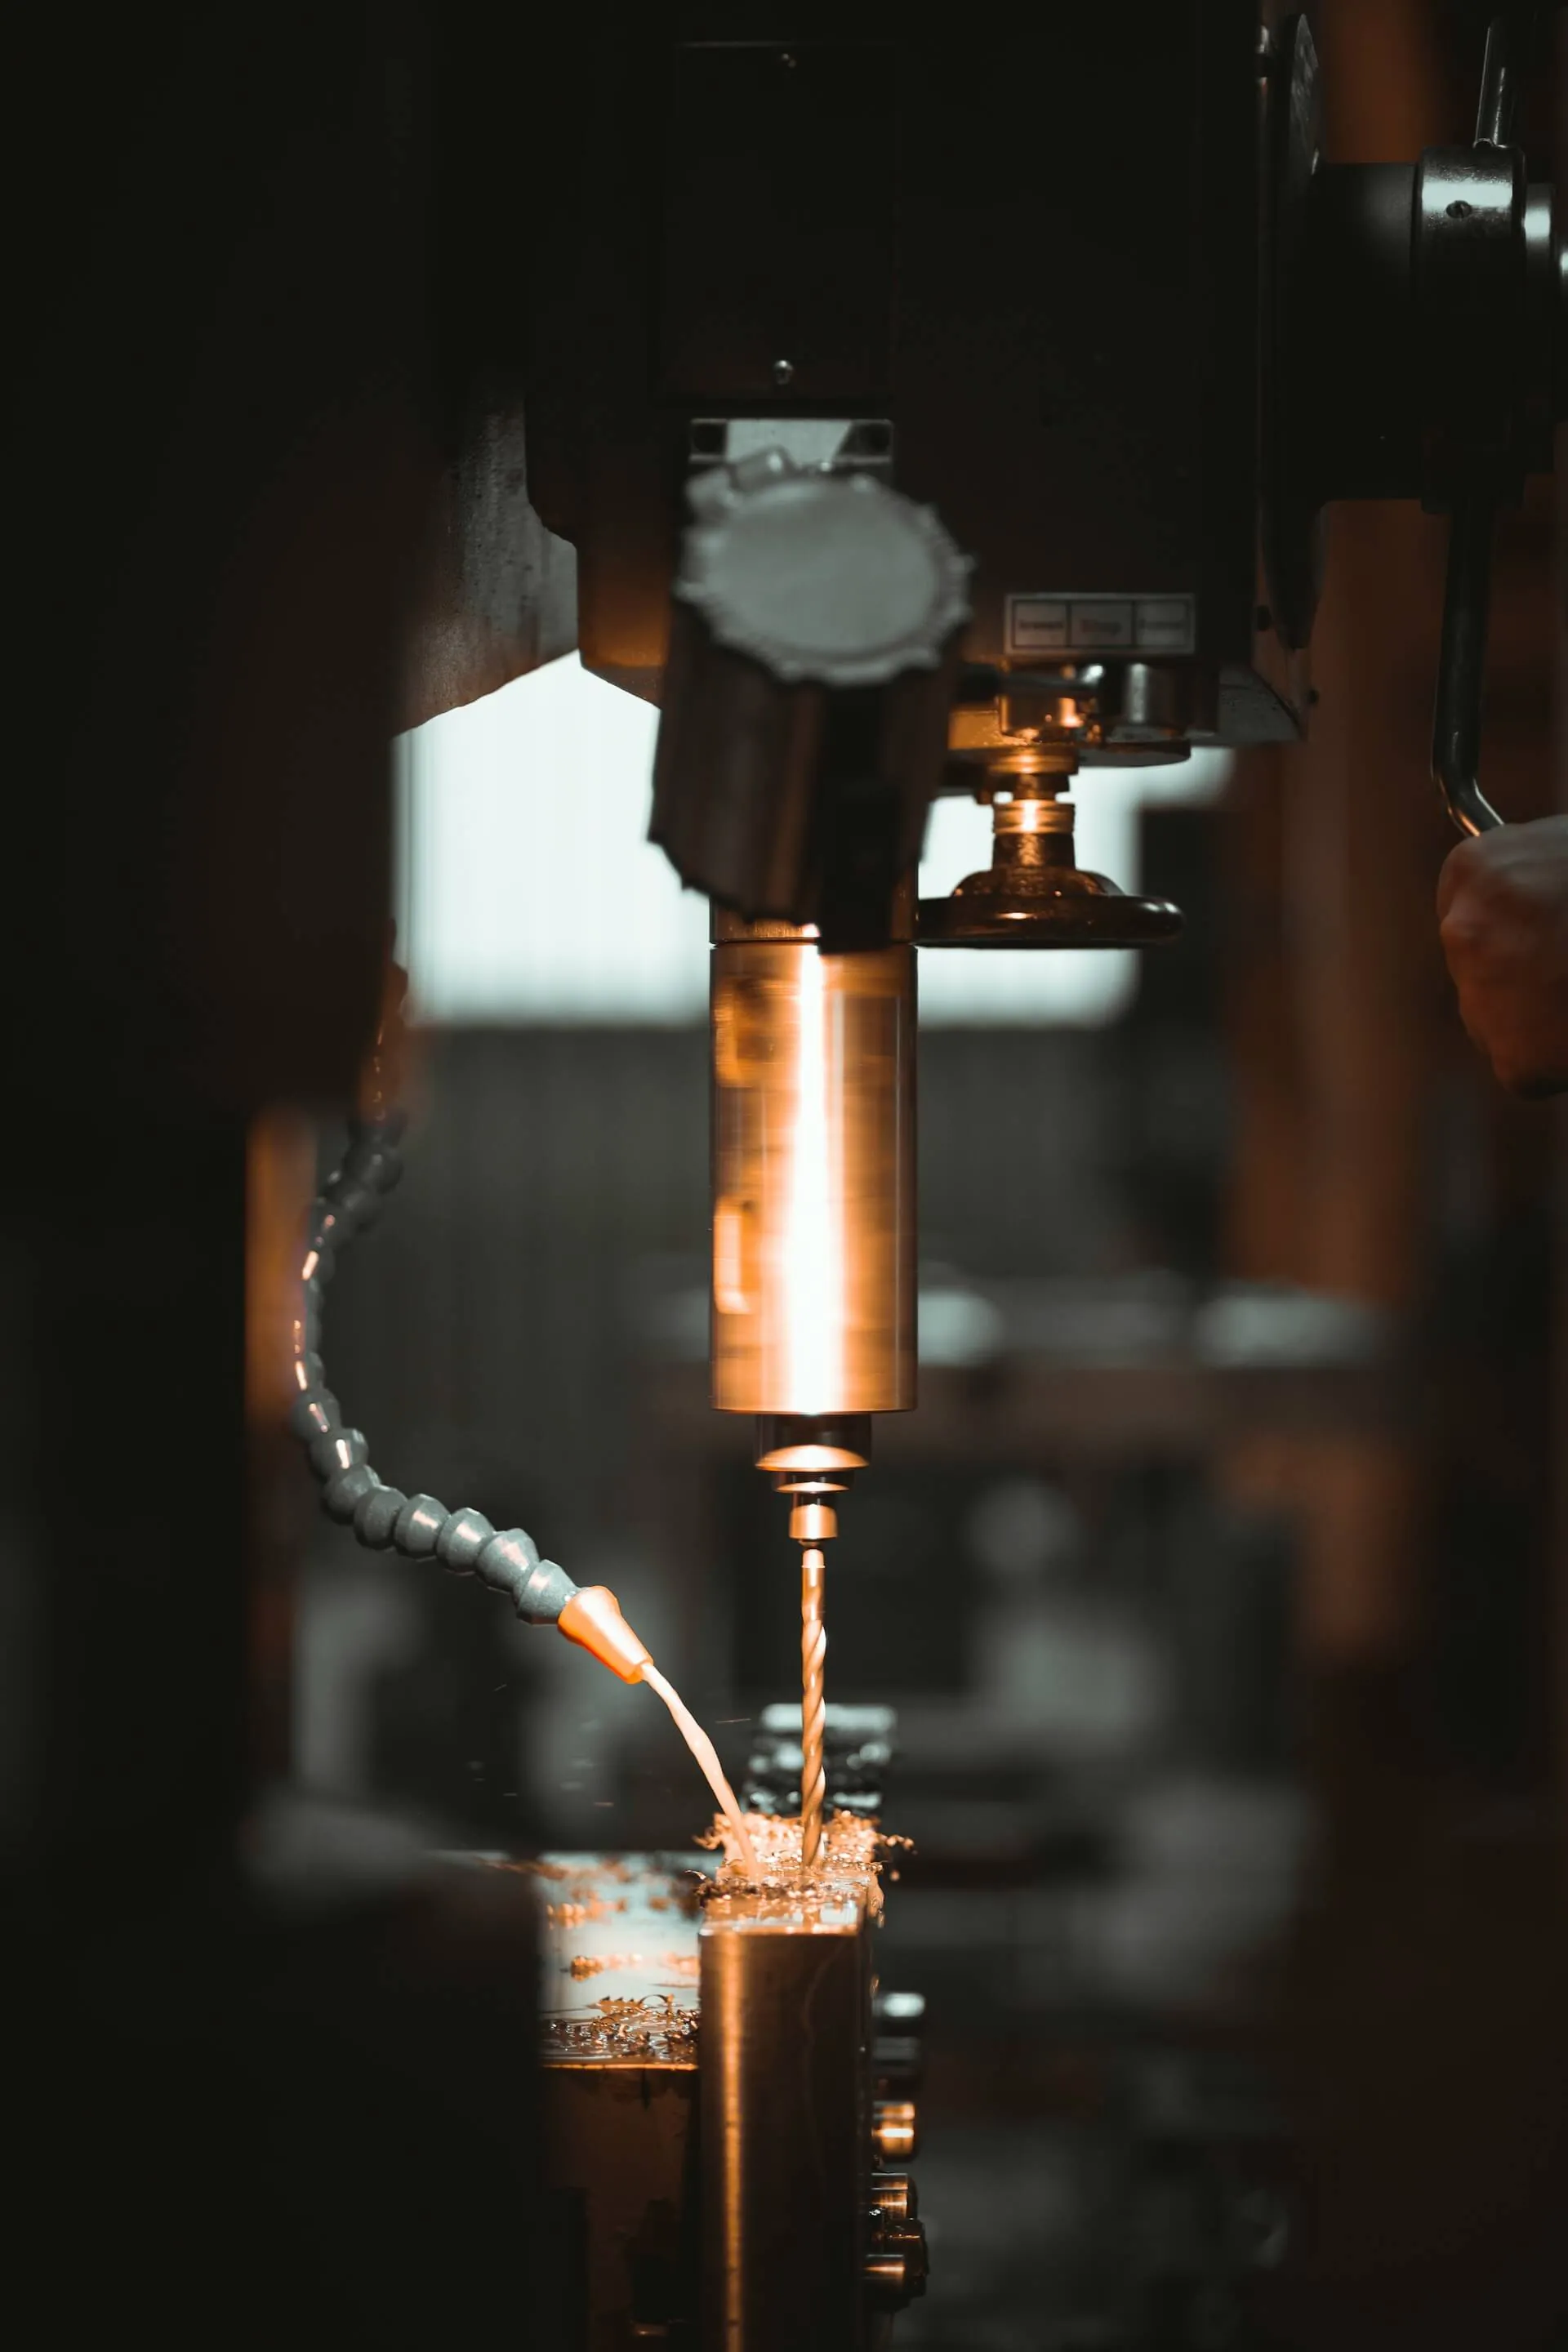
HAUSER machines for high-accuracy hole positioning.
- Work table 800 × 700 mm
- Drilling depth up to 140 mm
- Tolerances down to ±0.001 mm
-
05
EDM
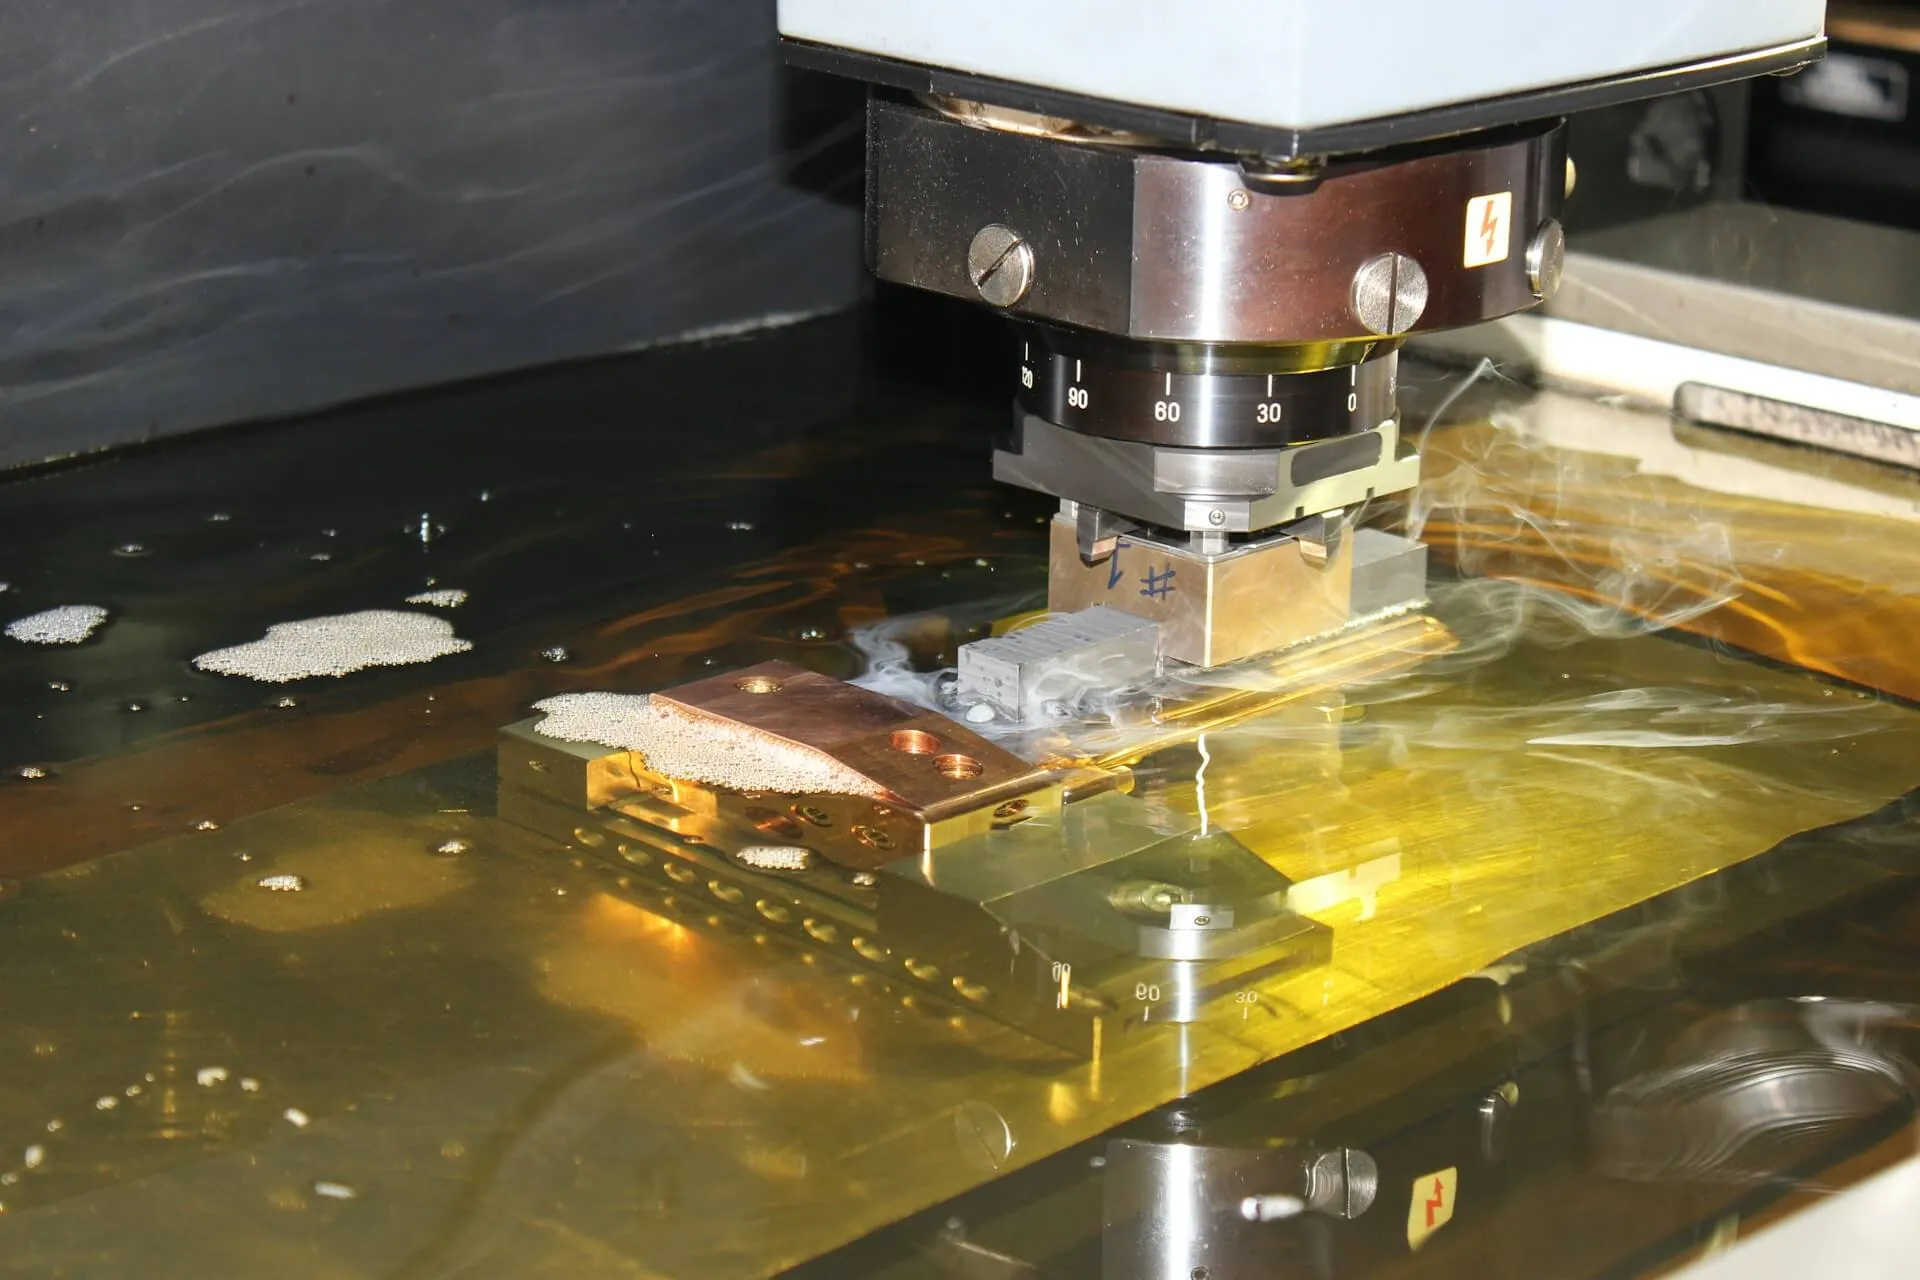
Sinker and wire EDM for complex cavities and hardened tool steels.
- Sinker EDM and wire cutting up to 500 × 350 mm
- Copper and graphite electrodes
-
06
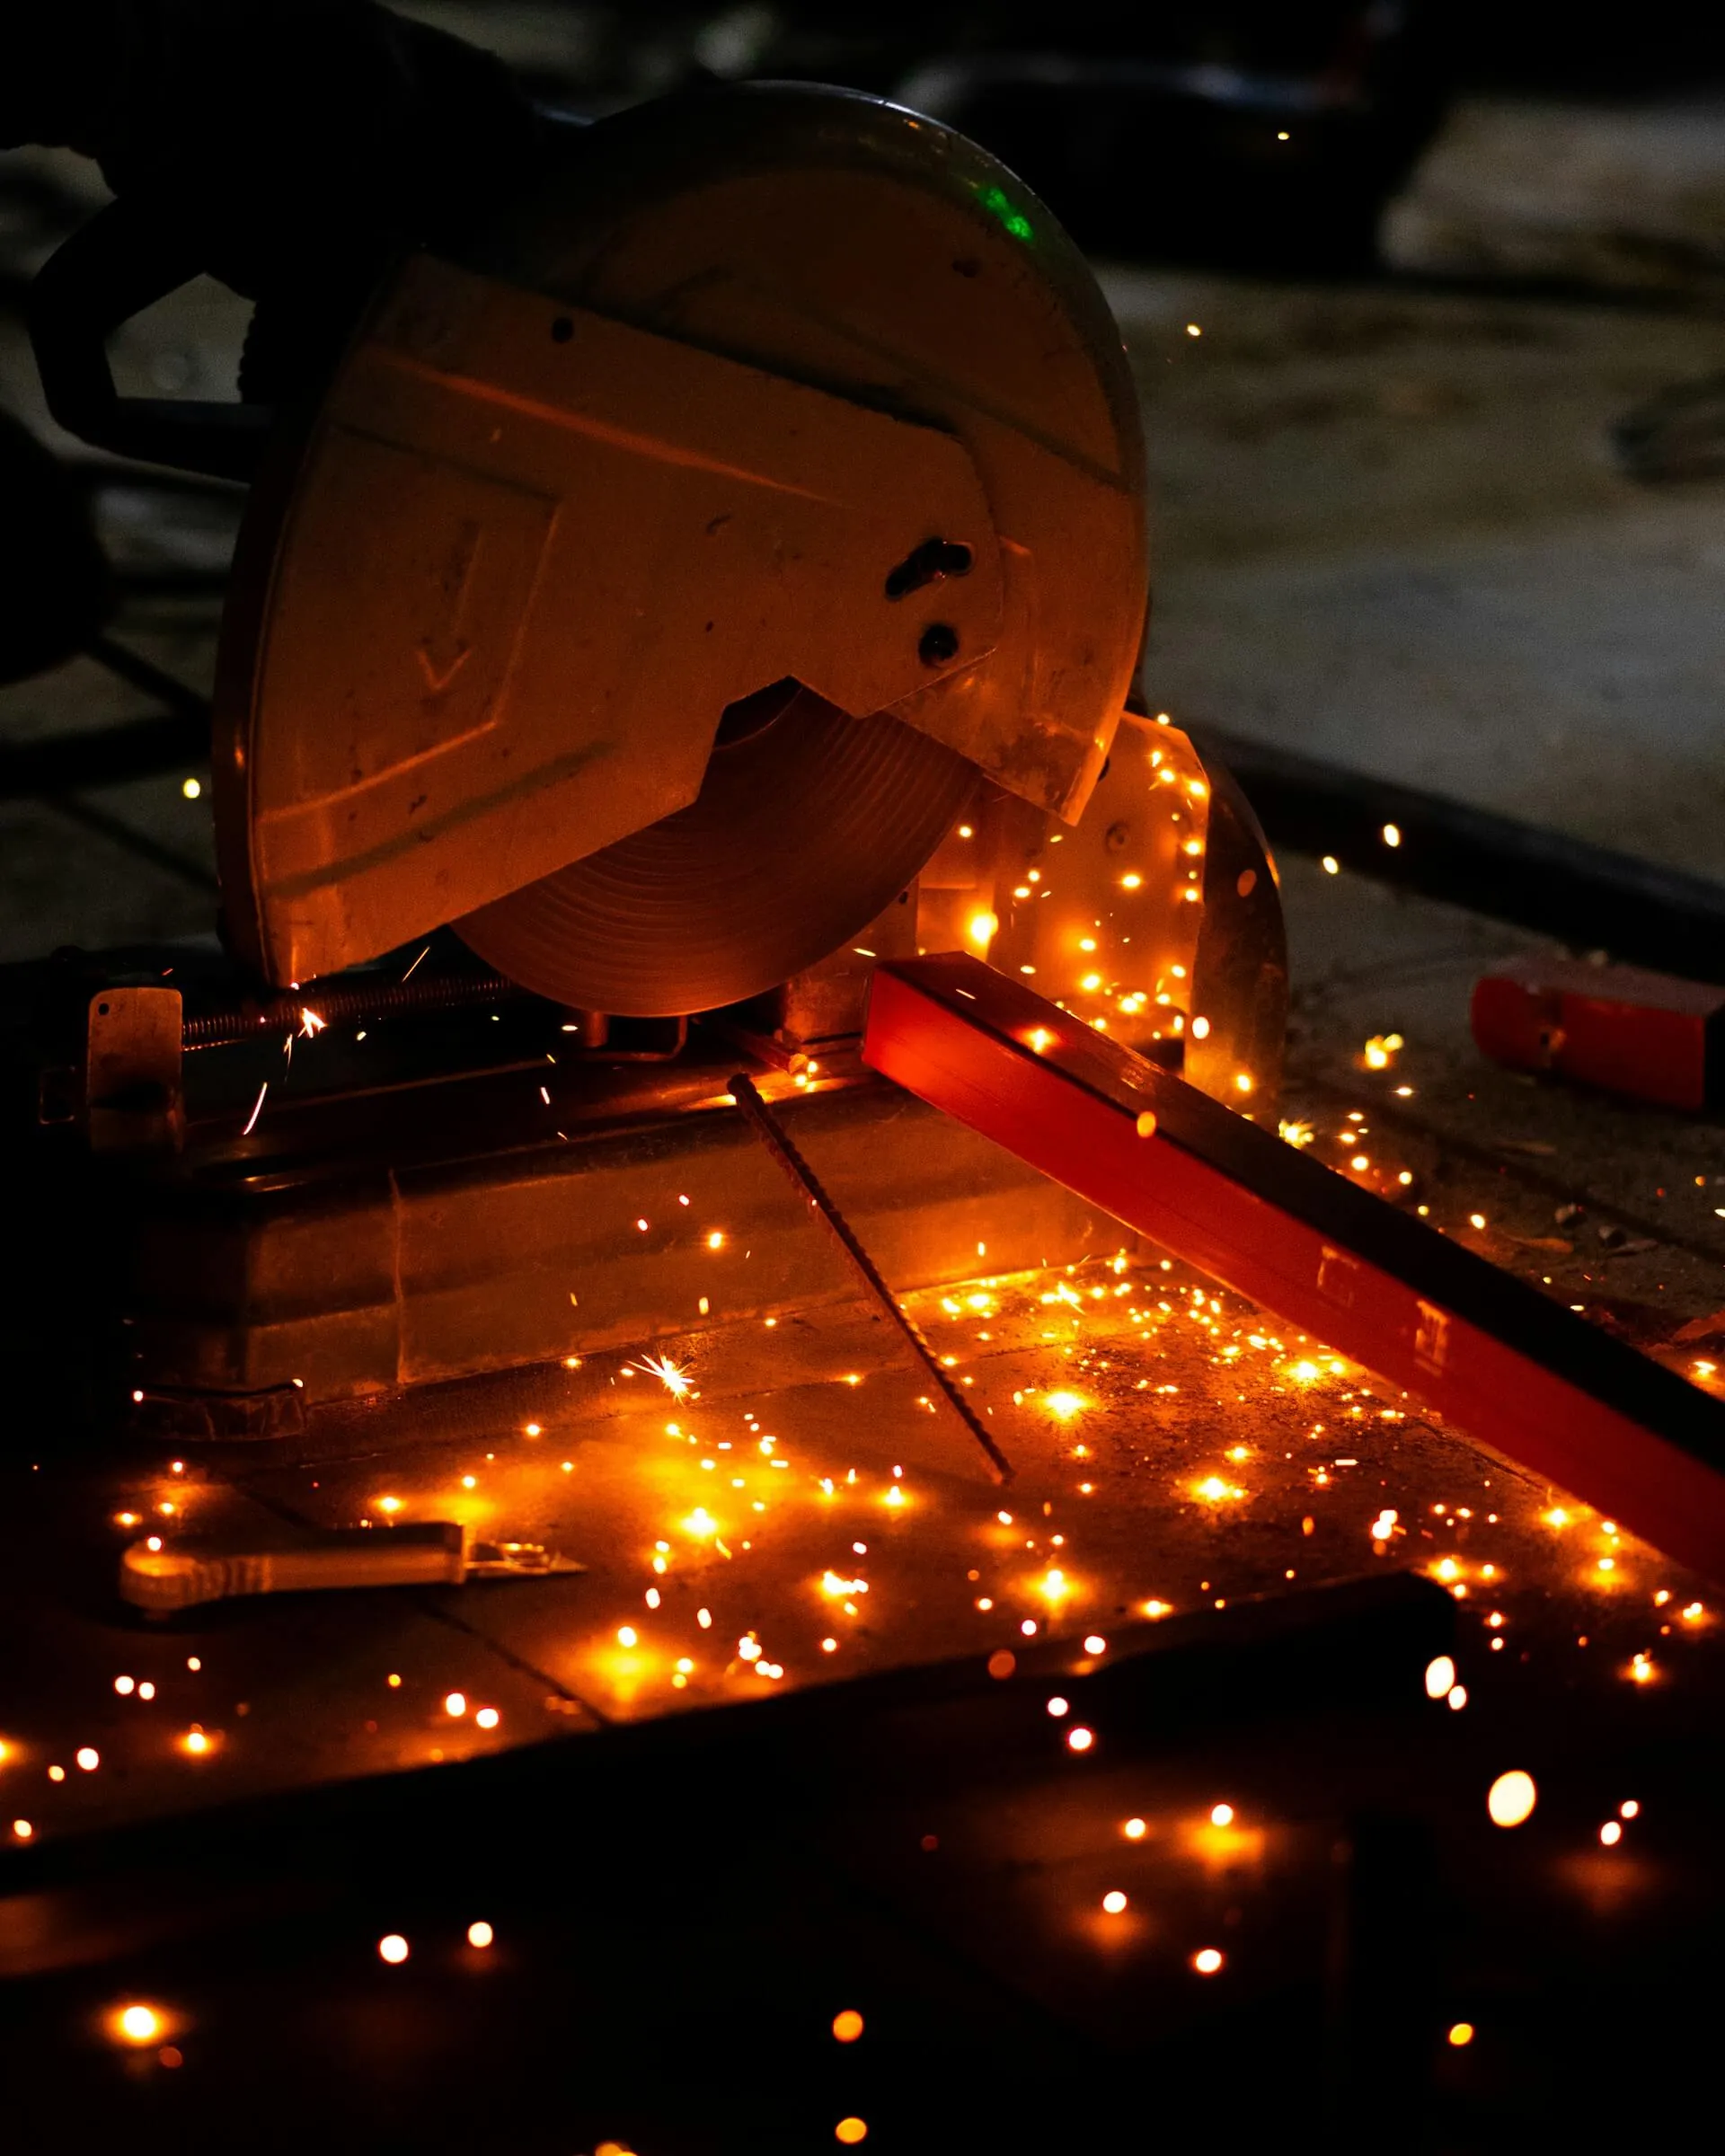
Cutting
Preparation of raw material before machining.
- Band saw for steel plates and profiles up to Ø400 mm
- Gas cutting
-
07
Presses
Production of sheet-metal parts and tool try-out.
- Eccentric presses up to 115 t
- Hydraulic press 600 t
-
08
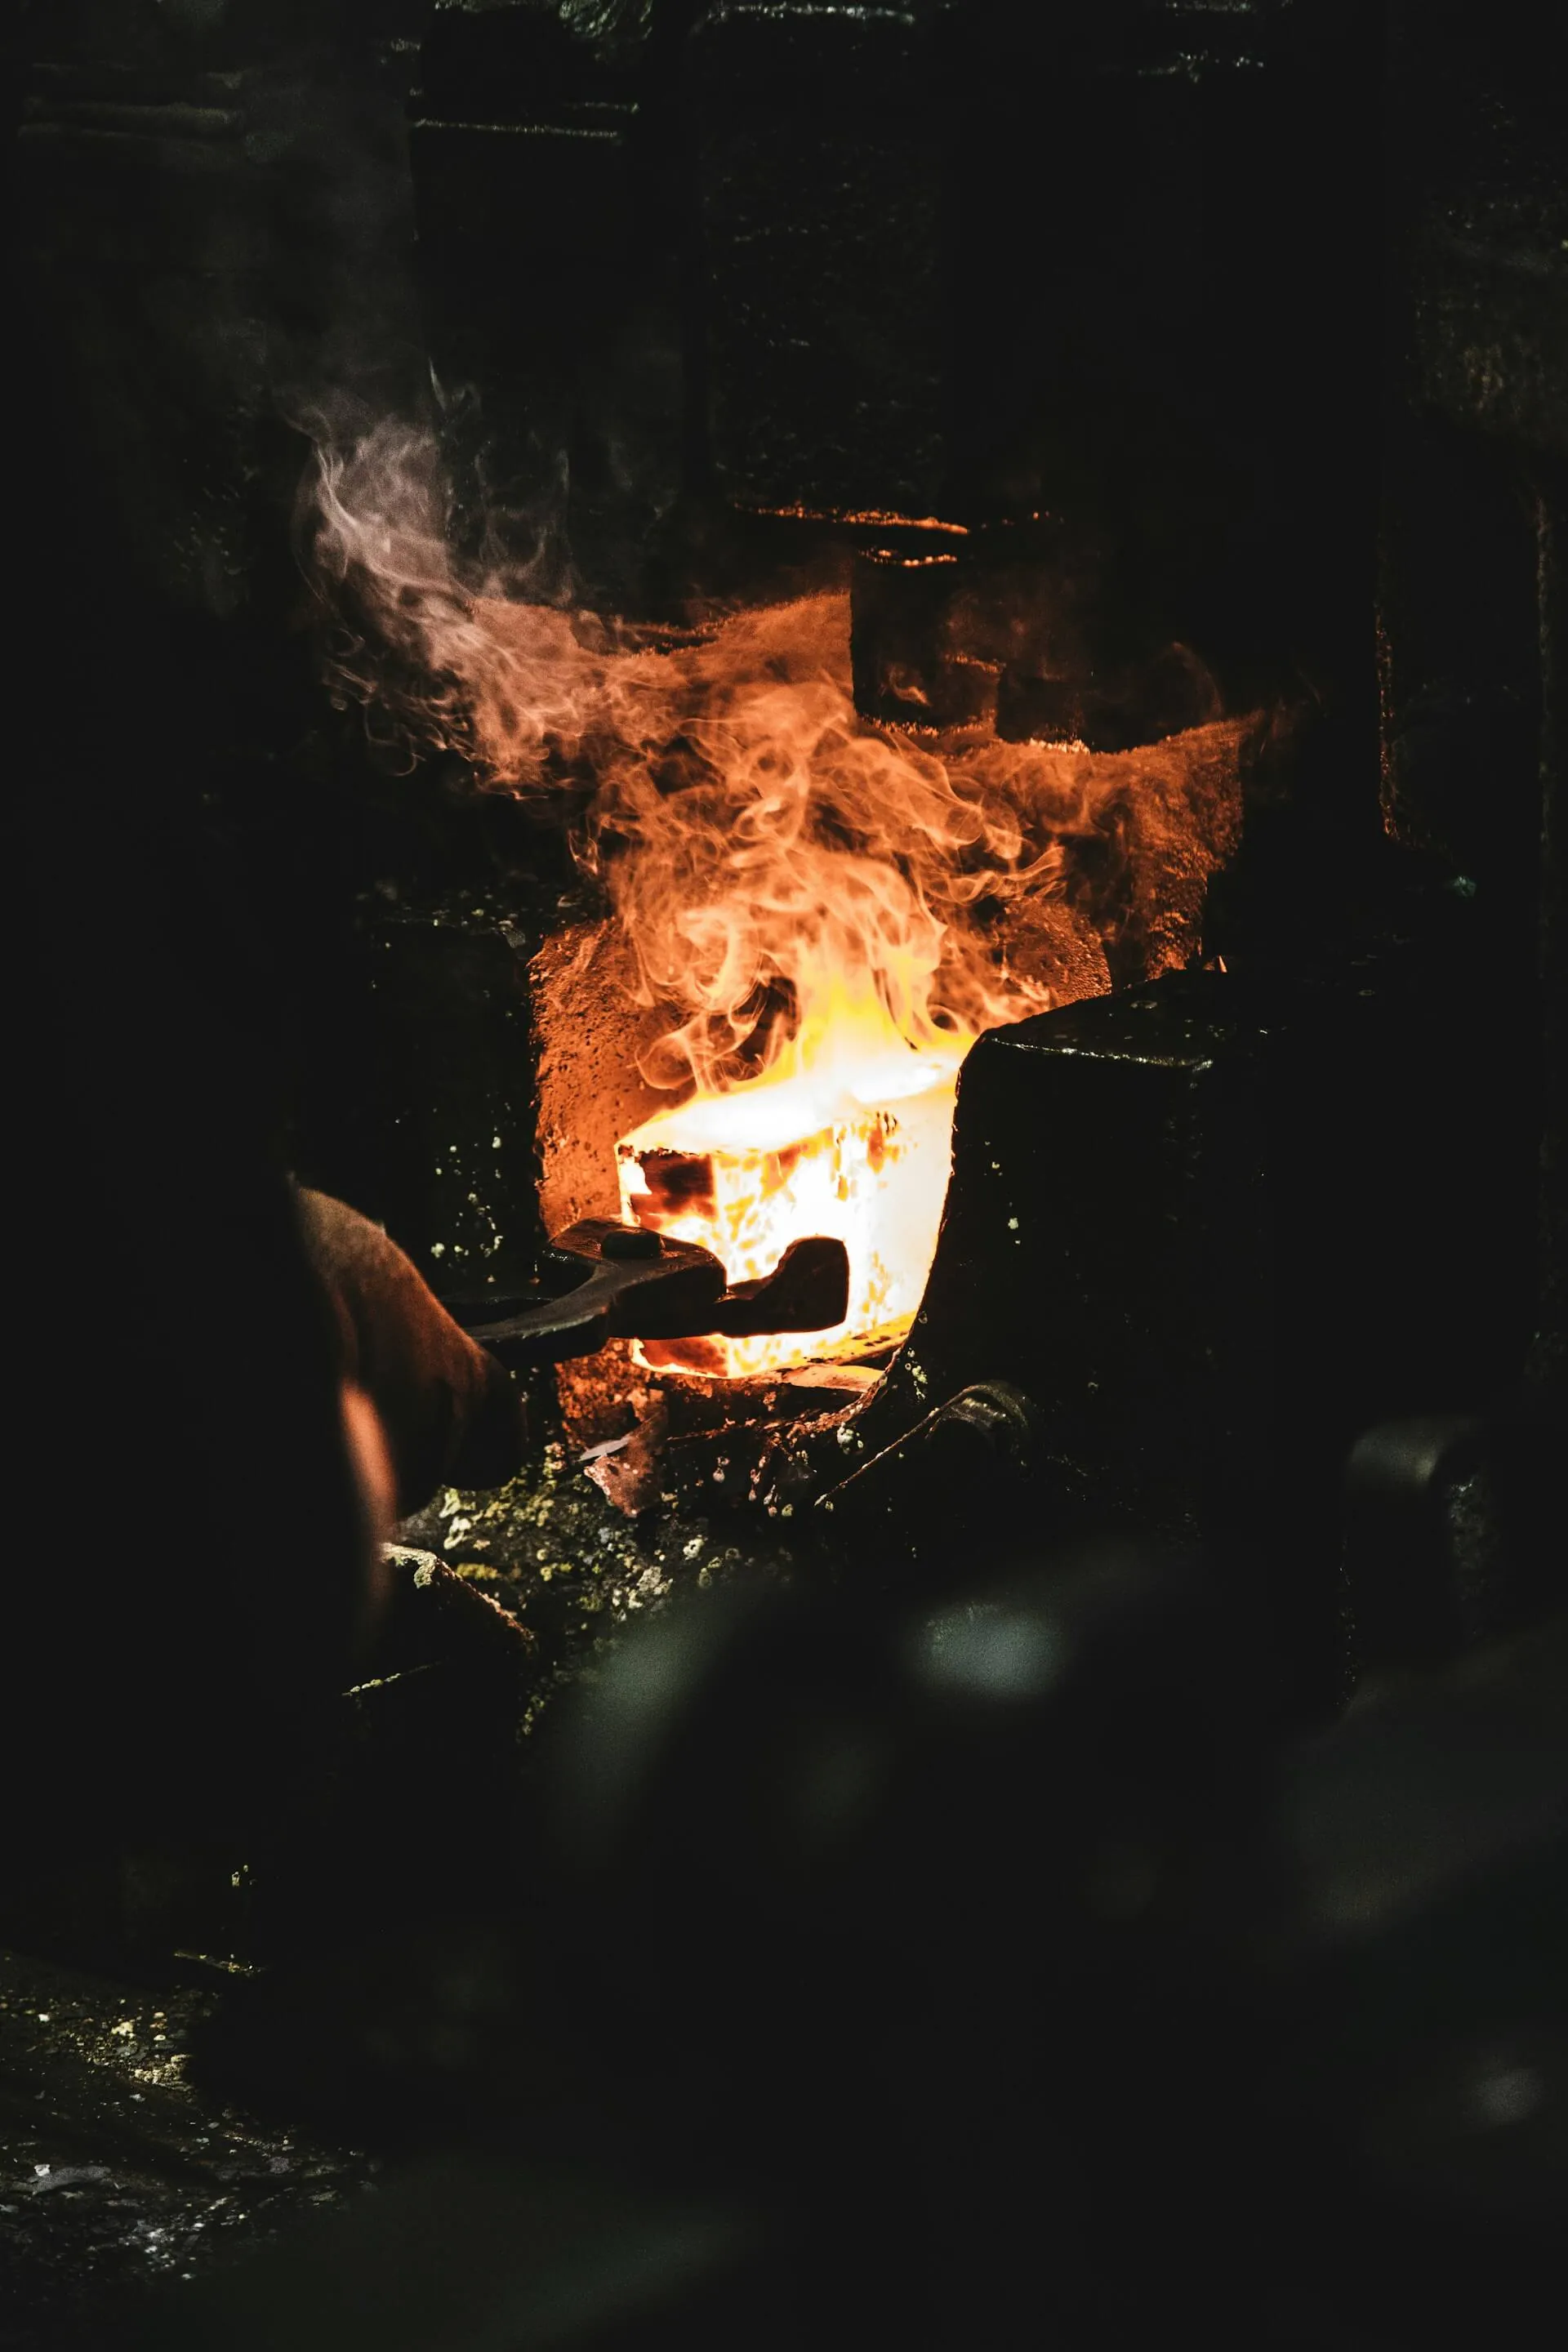
Heat treatment
Hardening of tool steels and steels for quenching and tempering.
- Hardening, tempering and case hardening
- Parts up to Ø150 × 400 mm
- Preparation of parts for heat treatment
-
09
Auxiliary operations
Repairs and finishing as part of the complete job.
- Minor welding and repair work on tools and supporting structures
- Polishing of functional surfaces to customer requirements
- Repair and refurbishment of existing tools
Specifications
Working ranges and tolerances
Key capacities of our machine park at a glance.
| Process | Working range | Tolerance |
|---|---|---|
| Jig grinding (HAUSER) | Table 800 × 700 mm | ±0.001 mm |
| Surface grinding | — | ±0.005 mm |
| CNC milling, 3-axis | 800 × 550 × 550 mm | ±0.01–0.02 mm |
| Conventional milling | 500 × 600 × 1,000 mm | — |
| Jig boring | Drilling depth up to 140 mm | — |
| Sinker & wire EDM | 500 × 350 mm | — |
| Band saw cutting | Up to Ø400 mm | — |
| Heat treatment | Up to Ø150 × 400 mm | — |
| Presses | Eccentric up to 115 t · hydraulic 600 t | — |
Achievable tolerances depend on the part’s geometry, the material and the machining process.
Materials
What we machine
- Tool steels 1.2379 · 1.2344
- Structural steels
- Stainless steels
- Aluminium alloys
- Non-ferrous metals
- Copper & graphite electrodes EDM
Working with a non-standard material? We make an individual technical assessment — send us your specifications.
Quality control
Measured at every step
- Dimensional and visual inspection after every operation
- Micrometers, calipers, height gauges and dial indicators
- Full geometry check and matching of tool assemblies before delivery
- Quality management certified to ISO 9001:2015
Have a project that demands precision?
Send us your drawings, CAD files or a sample — our team analyses your requirements and prepares a technical solution.